


Critical Quality Attribute (CQA) is essential in pharmaceutical manufacturing, directly impacting drug safety, efficacy, and consistency. As ICH Q8(R2) puts it, quality cannot be tested into products; it should be built in by design. Modern approaches like Quality by Design (QbD) emphasize early identification and control of CQAs to ensure robust drug development and manufacturing processes. ICH Q8(R2), which both FDA and EMA have adopted as guidance, expects pharmaceutical development to identify potential CQAs and to define a control strategy that keeps them within appropriate limits.
Adhering to Good Manufacturing Practices (GMP) ensures consistent monitoring and control of CQAs, reducing variability and safeguarding patient health. GMP frameworks integrate CQA management as a core component to maintain product integrity and comply with regulatory requirements. This systematic control supports pharmaceutical companies in delivering safe, effective, and reliable medicines to the market, fulfilling both patient needs and regulatory expectations.
Table of Contents
What is Critical Quality Attribute (CQA) in pharmaceuticals?
ICH Q8(R2) defines a critical quality attribute (CQA) as a physical, chemical, biological or microbiological property or characteristic that should be within an appropriate limit, range or distribution to ensure the desired product quality. CQAs are generally associated with the drug substance, excipients, intermediates and the drug product. In other words, if a CQA drifts outside its limits, the safety or efficacy of the medicine can be affected.
CQAs include many important factors, such as:
- Drug potency
- Purity levels
- Dissolution rate
- Sterility
- Stability
- Particle size
- pH level
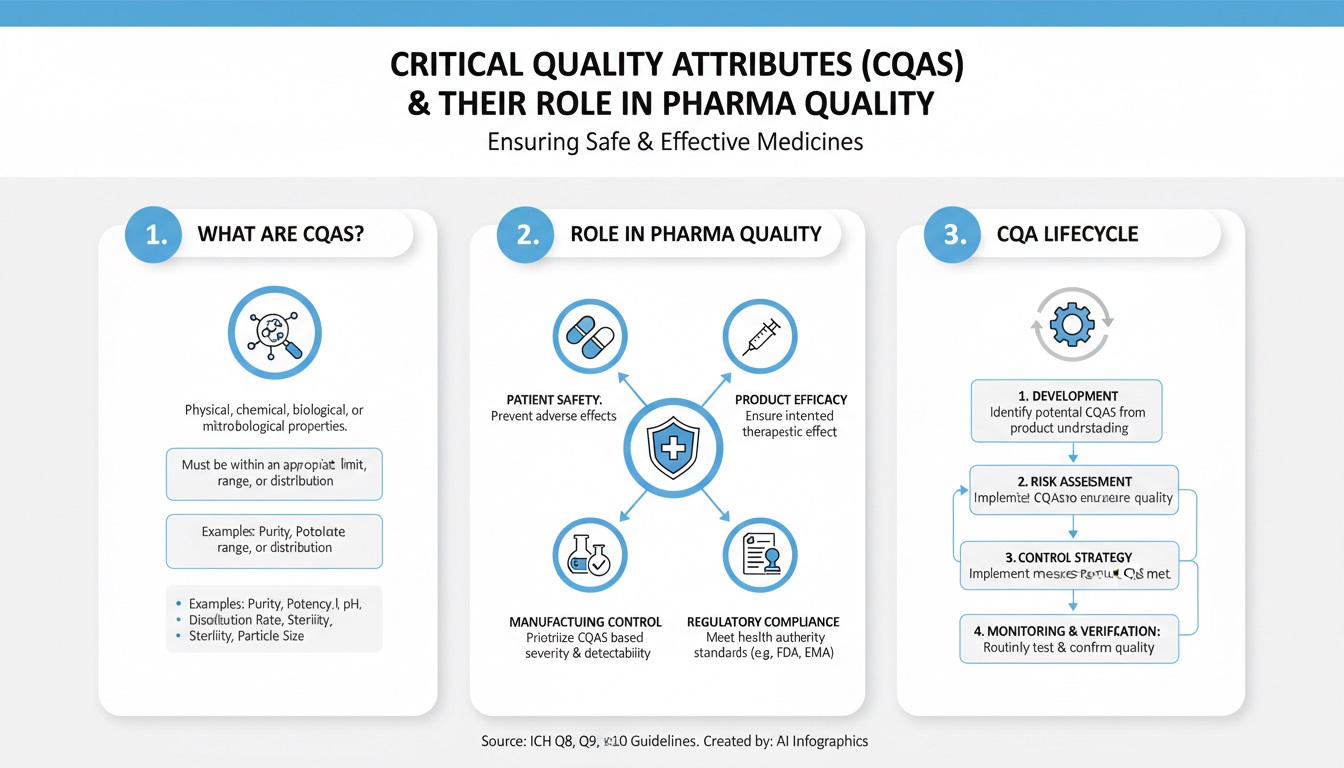
Examples of Critical Quality Attributes in pharma products
Critical Quality Attributes vary depending on the pharmaceutical product type. For example, CQAs of solid oral dosage forms typically cover purity, strength, drug release and stability. Other delivery systems add product-specific CQAs, such as aerodynamic properties for inhaled products, sterility for parenterals and adhesion for transdermal patches. Similarly, for drug substances and intermediates, properties such as particle size distribution or bulk density can be CQAs when they affect the finished product.
Moreover, solid oral dosage forms require uniformity in weight and hardness. Meanwhile, inhalers need particle size control for proper lung delivery. These examples show how CQAs change with drug forms but always focus on safety and effectiveness.
How to Identify and Define CQAs in Four Steps
To identify and define CQAs, start by understanding the product and process. Learn how the drug works and the manufacturing steps. Then, identify potential quality attributes that might affect safety or effectiveness. Next, assess the risk and impact of each attribute carefully to prioritize them.
Finally, define and document the CQAs clearly for future control and monitoring. These four steps help ensure high drug quality:
- Step 1: Understand the Product and Process
- Step 2: Identify Potential Quality Attributes
- Step 3: Assess Risk and Impact
- Step 4: Define and Document CQAs
Stepwise Approach to Defining CQAs with Key Activities
| Step | Description | Key Activity | Outcome |
|---|---|---|---|
|
1 |
Understand Product and Process |
Study product properties |
Clear understanding of product |
|
2 |
Identify Potential Attributes |
List attributes affecting quality |
Comprehensive attribute list |
|
3 |
Assess Risk and Impact |
Analyze impact on safety and efficacy |
Prioritized attribute risks |
|
4 |
Define and Document CQAs |
Record critical quality attributes |
Official CQA documentation |
Step 1: Understand the Product and Process
Start with the quality target product profile (QTPP), a prospective summary of the quality characteristics the drug product should achieve, taking safety and efficacy into account. It covers points such as route of administration, dosage form, strength, container closure system, drug release, and quality criteria like sterility, purity and stability. Potential CQAs are then derived from the QTPP and prior knowledge.
To understand the product and process, study all manufacturing steps carefully. Learn how each step impacts the final product. Also, consider the raw materials’ quality and source. Together, these factors guide you to define meaningful CQAs that ensure product reliability.
Step 2: Identify Potential Quality Attributes
Identify potential quality attributes by focusing on factors that affect product performance. Look at material properties and process parameters. Also, consider patient safety and regulatory requirements. Moreover, gather team input for a comprehensive view. Thus, you create a solid list for further analysis.
- Review product specifications carefully.
- Analyze manufacturing process steps.
- Check raw material characteristics.
- Consult with experts and stakeholders.
- Consider customer and regulatory needs.
Step 3: Assess Risk and Impact
Assess risk and impact by evaluating how each attribute affects product safety and quality. Use data and experience to rank the risks. Then, focus on attributes with the highest impact to ensure product success.
- Analyze historical data and trends.
- Evaluate potential safety concerns.
- Prioritize attributes based on impact and likelihood.
Step 4: Define and Document CQAs
Define and document CQAs clearly to ensure everyone understands their importance. Describe each attribute’s limits and why it matters. Also, record how you measure and monitor these attributes. This step helps maintain consistent product quality over time.
- List all critical quality attributes.
- Specify acceptable ranges for each attribute.
- Explain the impact on product safety.
- Detail measurement methods and tools.
- Assign responsibility for monitoring each CQA.
- Update documents as processes change.
Building a Control Strategy Around CQAs
Identifying CQAs is only half the job; the next step is to control them. ICH Q8(R2) describes a control strategy as a planned set of controls, derived from current product and process understanding, that ensures process performance and product quality. These controls should be based on product, formulation and process understanding, and at a minimum they should include control of critical process parameters and material attributes.
A control strategy can combine several elements: controls on input materials such as the drug substance, excipients and primary packaging; the product specification; controls for unit operations that affect downstream processing or quality, for example the impact of drying on degradation; in-process or real-time release testing instead of end-product testing; and a monitoring programme to verify prediction models. Each element can rely on a different approach, and the rationale should be described in the submission.
FDA and ICH Guidelines on Critical Quality Attributes
Regulatory agencies like FDA and ICH provide guidelines for managing Critical Quality Attributes. These guidelines help manufacturers ensure product safety and effectiveness. They explain how to identify, assess, and control CQAs throughout development and production.
For more details, download the FDA and ICH guideline PDFs below. Also, follow these guidelines to meet regulatory expectations and avoid delays.
Difference between Critical Quality Attribute (CQA) and Critical Process Parameter (CPP)
Critical Quality Attributes (CQAs) define the product’s quality and safety. In contrast, a critical process parameter (CPP) is a process parameter whose variability has an impact on a CQA and therefore should be monitored or controlled. CQAs focus on the end product, while CPPs focus on the process. Together, they ensure a consistent and high-quality product.
Moreover, CQAs measure product properties like purity and strength, while CPPs control variables like temperature and mixing speed. CQAs set the goal, and CPPs guide how to achieve it. Both require careful monitoring to meet quality standards.
Where Material Attributes and Real-Time Release Fit
CQAs do not depend only on process parameters. Material attributes, such as the particle size of the drug substance or the moisture content of a diluent, can also affect product CQAs. Risk assessment tools like an Ishikawa diagram combined with FMEA help teams rank these variables, and design of experiments can then show how they interact. As a result, the team learns which inputs need tight control and which do not.
With enough understanding, companies can move controls upstream. For example, ICH Q8(R2) notes that disintegration could serve as a surrogate for dissolution for fast-disintegrating forms with highly soluble drug substances. However, real-time release testing can replace end-product testing, but it does not replace the GMP review and quality control steps needed to release a batch.
Methods to monitor and control CQAs during pharma production
Process Analytical Technology (PAT) helps monitor CQAs in real time during production. It uses sensors and analyzers to measure product quality continuously. Also, PAT allows quick adjustments to keep the product within specifications. This method improves efficiency and reduces errors.
Similarly, Statistical Process Control (SPC) tracks data trends and detects variations early. It uses charts to visualize process performance over time. Operators act on SPC findings to prevent quality issues. Both PAT and SPC work together to ensure consistent pharmaceutical quality.
- Use PAT for real-time quality monitoring
- Apply SPC to track and control process variations
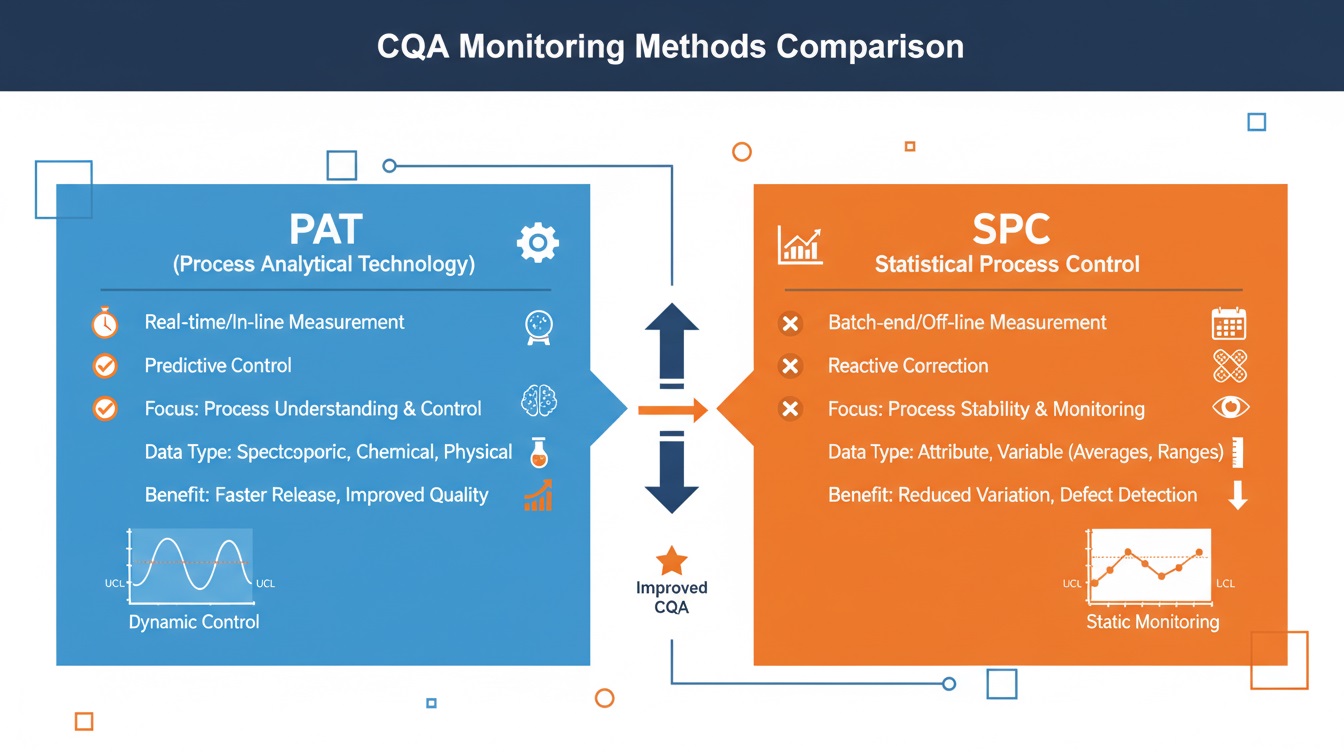
Process Analytical Technology (PAT)
The FDA’s PAT guidance helps companies apply Process Analytical Technology in manufacturing. It encourages real-time monitoring to control product quality during production. Also, this guide supports using sensors and analyzers to detect issues early and reduce waste.
Furthermore, the FDA guide promotes continuous improvement by integrating PAT with quality systems. It helps firms increase efficiency while ensuring safe, effective medicines.
Statistical Process Control (SPC)
Statistical process control fits naturally into the lifecycle approach to Process Validation in Pharmaceutical . FDA’s 2011 guidance describes Stage 3, continued process verification, as ongoing assurance during routine production that the process remains in a state of control. Similarly, EU GMP Annex 15 expects statistical tools to be used, where appropriate, to support conclusions about process variability and capability during ongoing process verification. Control charts of CQA results are a practical way to meet both expectations.
Final Word
Critical Quality Attributes (CQAs) are vital for pharmaceutical product safety and efficacy. ICH Q8(R2) adds that process performance can be monitored and trended during routine manufacture to confirm that the process delivers the expected quality attributes. Companies should prioritize risk assessment and real-time data analysis to effectively manage CQAs and prevent deviations during production.
Quality assurance relies on comprehensive CQA management to maintain high standards throughout the product lifecycle. The FDA emphasizes integrating quality assurance with continuous monitoring and process improvements. Implementing best practices like Statistical Process Control (SPC) further strengthens quality assurance efforts.
FAQs
A CQA is a physical, chemical, biological or microbiological property or characteristic that should stay within an appropriate limit, range or distribution to ensure the desired product quality. Typical examples are purity, strength, drug release and stability.
CQAs relate to product quality attributes, while CPPs control manufacturing process variables. Both must be monitored for consistent product quality.
Not necessarily. Under ICH Q8(R2), the specification is only one element of the control strategy. A CQA can also be assured through controls on input materials, in-process controls or real-time release testing, provided the rationale is justified in the submission.
Ershad Moradi
Ershad Moradi, a Content Marketing Specialist at Zamann Pharma Support, brings 6 years of experience in the pharmaceutical industry. Specializing in pharmaceutical and medical technologies, Ershad is currently focused on expanding his knowledge in marketing and improving communication in the field. Outside of work, Ershad enjoys reading and attending industry related networks to stay up-to-date on the latest advancements. With a passion for continuous learning and growth, Ershad is always looking for new opportunities to enhance his skills and contribute to pharmaceutical industry. Connect with Ershad on Facebook for more information.
Pharmaceutical Cold Chain Excursion: Causes, Impact, and a Practical Management Guide
A pharmaceutical cold chain excursion can threaten medicine quality, stability, and patient safety. Learn how to detect, document, assess, and manage temperature deviations using current guidance and science-based risk assessment.
Pharmaceutical Supply Chain: The Ultimate Guide to Hidden Risks and Challenges
Protocol deviations can threaten participant protection and trial reliability. This practical guide explains risk-based classification, documentation, escalation, CAPA, and preventive oversight.
Protocol Deviations in Clinical Trials: Build an Audit-Ready Record
Protocol deviations can threaten participant protection and trial reliability. This practical guide explains risk-based classification, documentation, escalation, CAPA, and preventive oversight.